If you’ve ever stood next to a large synchronous motor—you know, the kind that powers massive pumps, compressors, or rolling mills in mines, power plants, or chemical plants—you’ll get why installing it right isn’t just a box to check. I’ve been selling these bad boys for 12 years, and I can’t tell you how many times I’ve shown up to a job site where a contractor skipped a step or cut a corner, only to have the motor hum off-kilter, overheat, or worse, shut down mid-shift and cost the client hundreds of thousands of dollars in downtime. This isn’t a ceiling fan you can bolt on in 20 minutes. These motors weigh 20 tons, have precision-machined rotors that need to line up to the thousandth of an inch, and one tiny wrong move can turn a $500k piece of equipment into a paperweight. Let me break down exactly what we (as your supplier, that’s us) walk every client through to make sure the install goes right, no surprises. Large Synchronous Motor
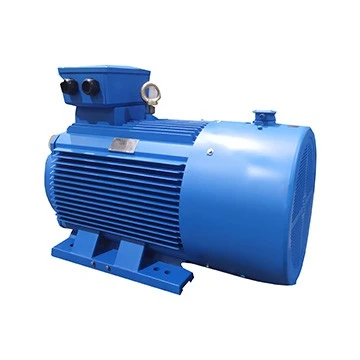
First off, pre-installation prep is non-negotiable—way more important than showing up with a crane and a crew. I see way too many teams showing up to the site first, then realizing the foundation is off, or the power feed isn’t strong enough, or they don’t have a spot big enough to fit the motor when they uncrating it. Let’s start with the foundation. I know it sounds basic, but 70% of the installation issues I’ve dealt with over the years trace back to a garbage foundation. You can’t just pour a concrete pad and call it good. This isn’t for a backyard shed. That foundation needs to be engineered specifically for that exact motor. Our team sends a dedicated field tech a full set of foundation specs 6 weeks before the motor is even scheduled to ship—no exceptions. That tech shows up to the site a full week before install day, not to lift the motor, but to verify every detail: the concrete cure time (you have to wait 28 full days for it to hit full strength, not 20 like some contractors think), the anchor bolt hole depth (they need to be 12x the bolt diameter, no skimping), the levelness (we check that with a digital level, not a bubble level—bubbles are for picnics, not critical installs), and the vibration resistance. If the foundation is even 0.005 inches out of level, that rotor is going to rub against the stator when it spins, and you’ll have a nightmare on your hands before you even flip the breaker. We don’t leave that to chance. If the foundation is off, we work directly with the client’s engineering team to fix it before any heavy lifting starts—saving everyone the hassle of tearing it apart mid-install.
Next up, uncrating and moving the motor to the install spot. I know it’s tempting to roll it off the shipping skid with a forklift, but those crates are built to protect the motor during transport, not to lift it off-site. Synchronous motors have delicate stator windings and precision rotor bearings that can get dinged if you yank them around. Our field techs use the exact lifting points we mark on every motor’s shipping crate—those are not generic. We put slings under the motor’s lifting lugs (never the stator housing, that’s for holding it steady, not lifting) and use a crane with a rated capacity 2x the motor’s weight. When we set it down on the foundation, we don’t just drop it and walk away. We use temporary shims—thin, precision-cut steel shims, not random pieces of wood or scrap metal—to get the motor’s base perfectly aligned. And we never let the motor sit on temporary shims longer than a day. Wood warps, metal shims can shift, and that’s when level goes out the window. We torque the anchor bolts in a specific crisscross pattern, too—no tightening one bolt all the way before moving to the next. That prevents warping the motor base, which would mess up the alignment later.
Now the big one: alignment. This is where 90% of avoidable post-install problems happen, and I can’t stress this enough—alignment is not guessing. There are two types you have to nail: shaft alignment and air gap alignment. Let’s start with shaft alignment: lining up the motor’s shaft with the driven equipment (say, a pump or compressor) that’s going to spin with it. Most guys use a dial indicator for this, and that’s the right move, but so many people rush it. The alignment needs to be within 0.001 inches per foot of shaft length—if you have a 10-foot shaft, that’s 0.01 inches total gap between the motor and the driven equipment. We do what’s called a “hot alignment” too, which means we run the motor for 20 minutes to get it up to operating temperature, then check alignment again. Metal expands when it heats up, so if you align it cold, once it’s hot, the shafts will be misaligned, causing vibration and bearing failure. I’ve seen a client skip hot alignment, run the motor for 3 hours, and blow a $20k bearing—all because they cut 30 minutes of work. That’s a rookie move we never let our clients make.
Then there’s air gap alignment—this is specific to synchronous motors, not just any motor. The air gap is the tiny space between the rotor and the stator, and it has to be exactly the same all the way around, within 0.002 inches. If it’s even a little off, the rotor will pull to one side when it’s energized, causing uneven magnetic pull, vibration, and even stator winding damage. How do we check that? We use feeler gauges, but not just shoving them in. We take measurements at 4 points: top, bottom, left, right of the rotor, every 90 degrees around the circumference. We do this while the rotor is sitting in the stator, not before we lower it in. If the gap is off, we adjust the motor’s shims (not the driven equipment) to fix it. This is tedious work—we spend 2-3 hours just on air gap alignment for a large motor—but it’s the difference between a motor that runs for 20 years without issues and one that needs a rebuild in 2 years. I once had a client who skipped checking air gap, got the motor fired up, and within 10 minutes there was a loud grinding noise. We had to pull the rotor back out, and the stator had a scratch that cost $15k to repair—all because they wanted to save a few hours. That’s not a win for anyone.
Once alignment is done, it’s time for electrical checks, and this is where a lot of electrical contractors drop the ball. Synchronous motors run on high voltage (usually 4kV, 6kV, even 11kV for large models), so cutting corners here is not just bad—it’s dangerous. First, we do an insulation resistance test (IR test) on the stator windings, using a megohmmeter. The insulation resistance needs to be at least 1 megohm per kV of operating voltage, and it has to stay consistent for 60 seconds. If it’s lower than that, there’s moisture or a flaw in the windings, and running the motor will burn them out. We also do a polarization index (PI) test, which is just the ratio of insulation resistance after 10 minutes vs. after 1 minute. A good PI is above 2. If it’s less than 1.5, that means there’s contamination in the windings, and we need to dry them out before powering up. I can’t tell you how many times we’ve found moisture in the windings because the motor was left exposed to rain during install—one of the first things we tell clients is to keep the motor’s terminal box and stator covers sealed until every other part of the install is done.
We also check the excitation system, which is what makes synchronous motors unique—they need DC power to energize the rotor, which gives them their power factor correction ability. We test the excitation voltage and current before connecting it to the grid, making sure it matches the specs we provided. If the excitation is too low, the motor won’t pull the load; too high, and you’ll waste energy or damage the rotor winding. We also make sure all the ground connections are tight and properly sized—bad grounding can cause electrical noise that messes up the motor’s controls, or even cause a shock hazard. Last thing we do before energizing is a complete visual walkthrough: check all bolts are torqued, all wires are secure, no tools left lying around on the motor (I’ve seen that more than once—someone left a wrench, and when the motor spun, it punched a hole in the stator), and all safety guards are in place. No shortcuts here.
Now, the final step: commissioning and testing the motor under load. A lot of contractors will just flip the breaker and run it idle for 10 minutes, but that’s not enough. We recommend running the motor at 25% load for an hour, then 50% for another hour, then full load for 4 hours. While it’s running, we monitor every key metric: vibration (we use a vibration analyzer that measures amplitude at different frequencies—anything over 0.1 inches per second is a red flag), temperature of the bearings and stator windings (bearings should stay under 100C, windings under 120C for most models), and current draw. If something is off during load testing, we catch it before it’s connected to the driven equipment, so we don’t shut down a whole plant. I had a client once skip full load testing, connect the motor to a compressor, and after 2 hours, the compressor overloaded and shut down, taking the whole production line with it. We fixed the motor in a day, but the client lost $200k in downtime—all because they wanted to rush the process.
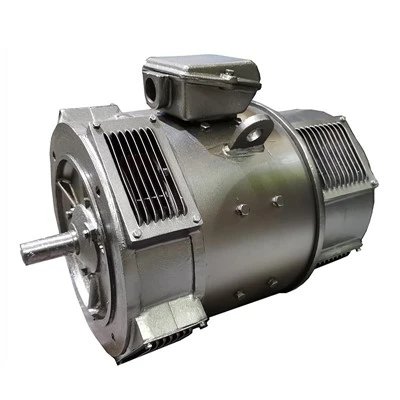
Here’s the thing: as a large synchronous motor supplier, we don’t just drop the motor at your site and vanish. We’re with you every step of the way, from pre-install checks to post-commissioning follow-up. We’ve seen every mistake there is—we’ve seen motors installed with dirt in the air gap, foundations that were too weak, alignment that was off by a tenth of an inch—and we’ve learned exactly how to prevent them. Installing a large synchronous motor is an investment, and you don’t want to cut corners on that investment. If you’re gearing up for a project that needs one of these workhorses, or you’re having issues with a motor that’s not running right, reach out to our team to chat. We’ll walk you through every step, answer all your questions, and make sure your motor runs smoothly for years.
AC Motor Reference
- IEEE Std 112-2017, Standard Test Procedure for Polyphase Induction Motors and Generators
- NEMA MG 1-2022, Motors and Generators, Part 2: Synchronous Motors
- American Society of Mechanical Engineers (ASME) PCC-1-2010, Guidelines for Coupled Shaft Alignment
Xian Putai Electric Motor Equipment Co., Ltd.
Xian Putai Electric Motor Equipment Co., Ltd. is one of the most professional large synchronous motor manufacturers and suppliers in China, also supports customized service with low price. Welcome to buy advanced large synchronous motor in stock here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: Haibo Guangchang Fengcheng Nine Road Economical & Technological Development District Xi’an City Shaanxi Province – China
E-mail: sales@putaimotor.com
WebSite: https://www.putaimotor.com/
